Choosing a valve actuator is rarely a simple catalog decision. Process conditions, control demands, safety functions, and maintenance resources must align. This is where Valve Automation becomes a practical engineering discipline, not merely a purchasing exercise.
Béla G. Lipták, a respected process-control authority, wrote, “The control valve is the final control element.” That statement deserves attention. A polished control strategy can still fail at the pipeline if the valve moves slowly, loses position, or cannot deliver enough torque. The right system should match the valve type, operating pressure, fluid temperature, cycling frequency, and required response time. Check torque margins carefully. Small errors become expensive stoppages.
The following seven Valve Automation tips focus on decisions engineers often face in real facilities. They examine actuator sizing, fail-safe behavior, power availability, feedback signals, environmental protection, diagnostics, and lifecycle maintenance. A dusty outdoor installation may need stronger enclosure protection than a clean indoor skid. A corrosive process may demand different materials and sealing methods. A high-cycle valve may punish an actuator chosen only by its initial price.
No selection guide can replace field experience. A checklist may overlook vibration, poor air quality, or limited technician training. That is an uncomfortable truth. It should encourage better questions, not false confidence. Compare supplier data with actual operating history. Test the complete valve, actuator, controls, and feedback loop together. The best system is not always the most advanced one. It is the one that performs reliably when conditions become inconvenient.
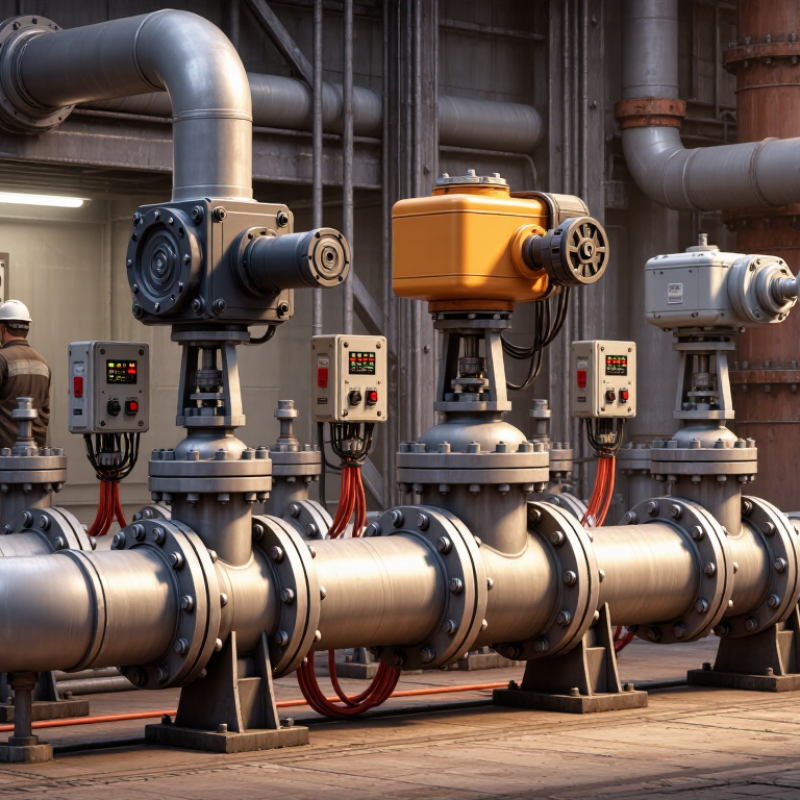
A valve automation system combines several working parts. The valve controls fluid movement through a pipe. The actuator supplies the movement needed to open or close it. Electric, pneumatic, and hydraulic actuators suit different operating conditions.
A positioner adjusts actuator movement according to the control signal. Feedback devices confirm the valve’s actual position. Solenoid valves direct air in pneumatic systems, while limit switches report open or closed status. Power supplies, wiring, and control panels connect these parts. Small failures can stop the entire process.
Tip 1: Match actuator torque with the valve’s real operating load. Do not rely only on catalogue estimates. Temperature, pressure, corrosion, and frequent cycling can change performance.
Tip 2: Check the fail-safe action during a power or air failure. The valve may need to close, open, or hold its position.
Tip 3: Select feedback equipment that operators can test easily. Clear signals reduce troubleshooting time.
During commissioning, I prefer a full stroke test under realistic conditions. Watch for delayed movement, air leaks, unusual noise, or unstable positioning. A dry workshop test is useful, but it cannot reveal every field problem. I once underestimated cable routing around a hot pipe, creating avoidable maintenance work. That mistake reinforced a simple lesson: installation details matter as much as component selection. Keep manuals, test records, and calibration dates accessible. Reliable automation depends on disciplined maintenance, not only sophisticated hardware.
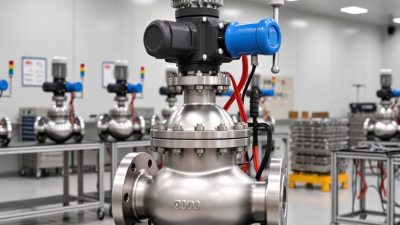
Defining process requirements before selecting a valve automation system prevents expensive misalignment. Start with the medium, pressure, temperature, flow direction, and required valve position. Tip: Record real operating conditions, not only design values. Field measurements often reveal pressure spikes, corrosion, or cycling that specifications miss. Also define failure behavior. Should the valve fail open, fail closed, or hold position during power loss? That choice affects safety, production continuity, and actuator sizing.
Tip: Measure cycle frequency and response time. A valve moving twice daily has different requirements from one operating every few seconds. Tip: Check available utilities, including air quality, voltage, and network capacity. Tip: Identify the control signal and communication protocol before procurement. According to McKinsey’s maintenance analysis, predictive maintenance can reduce machine downtime by 30–50% and maintenance costs by 10–40%. However, automation data is useful only when sensors, diagnostics, and operating limits are clearly defined.
Tip: Map the installation environment. Dust, moisture, vibration, and hazardous-area classifications can change enclosure and protection requirements. Tip: Ask operators to describe manual interventions, unusual noises, and recurring delays. Their experience may expose risks that drawings overlook. Tip: Specify maintenance access, spare-part expectations, and testing procedures. Deloitte’s 2023 Smart Manufacturing and Operations Survey found that 86% of manufacturers view smart manufacturing as important to competitiveness. Yet digital features should not replace basic process understanding. I have seen projects overvalue connectivity and undervalue simple, reliable valve movement. That mistake deserves a second review.
The chart presents a reference process specification for an automated quarter-turn valve application. Confirming pressure, temperature, flow, valve size, cycle time, required torque, control signal, and environmental protection before selection helps ensure reliable operation and correct actuator sizing.
Matching valve types, actuators, and control methods begins with the process, not the catalog. A quarter-turn ball or butterfly valve suits fast isolation, while a globe valve offers finer throttling. Check pressure drop, temperature, media viscosity, and required shutoff class. The 2024 Grand View Research Industrial Valves Market Report valued the global market at approximately USD 78.7 billion in 2023, showing how broad—but not simple—the selection landscape has become.
Size the actuator from real torque, not nominal valve diameter. Include breakaway torque, packing friction, differential pressure, and a safety margin. Pneumatic actuators remain practical where compressed air is reliable. Electric actuators can improve positioning and diagnostic access. Hydraulic units may fit large valves or remote installations. IEC 60534 guidance supports control-valve sizing, but field conditions can still defeat a perfect calculation. I have seen undersized actuators stall during cold starts.
Match the control method to operating risk. On-off service may need limit switches, position feedback, and emergency action. Modulating service usually requires a positioner, calibrated signal, and stable control logic. Specify fail-open, fail-closed, or fail-in-place behavior after reviewing the process hazard study. The U.S. Department of Energy reports that compressed-air systems can lose 20%–30% of output through leaks and poor maintenance. That matters. Test signal response, inspect air quality, and document valve travel. A small commissioning error can become a costly shutdown. Recheck assumptions.
Evaluating Safety, Reliability, and Environmental Performance
A suitable valve automation system should protect people before it improves production speed. Review shutdown behavior, actuator response time, and accessible emergency controls. A fail-safe position must match the process hazard, not simply the equipment supplier’s default setting. Test the complete valve assembly under realistic pressure and temperature conditions. Laboratory results can mislead when field conditions vary.
Reliability depends on more than a strong actuator. Check cycle ratings, diagnostic coverage, enclosure protection, and resistance to vibration. Confirm that control signals remain stable during power interruptions. Maintenance teams should reach critical components without entering unsafe areas. Keep spare parts practical. I have seen systems fail because one small seal was unavailable for weeks. That detail deserves attention.
Environmental performance needs measurable evidence. Inspect compressed-air consumption, fugitive emissions, noise levels, and energy use during partial loads. Choose materials that tolerate chemicals without creating premature waste. Record leakage rates during commissioning and routine inspections. Small leaks become expensive over time. However, lower energy use does not automatically mean better performance. A weak actuator may consume less energy while causing process instability and repeated replacement. I still question designs that rely on ideal weather, perfect calibration, or constant operator attention. Real plants are messier. Their automation systems should be tested accordingly.
Integration should guide valve automation decisions, not the initial equipment price. Map every actuator, control signal, network protocol, and existing cabinet connection. Confirm compatibility before requesting quotations. A small interface mismatch can create expensive engineering work later. Require open communication standards and documented data points. Also check whether technicians can access diagnostics without stopping the process.
Maintenance needs deserve equal attention. Choose assemblies with visible position indicators, replaceable seals, and accessible calibration points. Ask about local spare parts, inspection intervals, training, and remote fault reporting. Keep records simple. Complex software often becomes unused software. The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide reports that predictive maintenance may reduce costs by 8–12% compared with preventive maintenance. Results vary by application. That warning matters.
Calculate total ownership costs across ten years. Include installation, configuration, energy use, planned shutdowns, cybersecurity updates, spare parts, and disposal. McKinsey’s 2018 maintenance analysis estimates predictive maintenance can reduce downtime by 30–50% and maintenance costs by 20–30%. These are industry estimates, not promises. Test them against your plant’s failure history. A pilot on critical valves can expose weak assumptions before a full rollout. Do not ignore training. A technically advanced system still fails when operators cannot interpret alarms. Perfect planning is rare. Review the decision after six months.